If you’ve ever worked with heavy industrial machinery, automotive components, or aerospace parts, you know that the line between a part that works reliably for 10 years and one that fails prematurely often comes down to something invisible to the naked eye: surface integrity. As a forging part machining supplier, I see this play out every single day in our shop floor. We take rough, hot-forged blanks, machine them to tight tolerances, and watch as client after client comes back with stories of parts that hold up or crack because of the work we did (or didn’t do) on their surfaces. Today, I want to break down what surface integrity really means for machined forging parts, why it matters more than just dimension accuracy, and the non-negotiable requirements we stick to here at our shop. Forging Part Machining
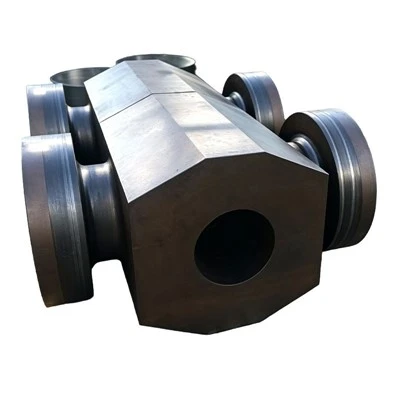
Let’s start with the basics: surface integrity isn’t just how smooth a part feels when you run your finger over it. It’s the combination of surface roughness (that’s the tiny, microscopic peaks and valleys left by machining), surface microstructure changes, residual stresses, and even microcracks that can form during the machining process. For forged parts specifically, this is extra critical because forging already creates a unique grain structure—usually elongated along the forging flow lines—that gives the part its strength. But when we machine that forging, we can accidentally damage that grain structure or introduce stresses that undermine everything the forging process worked to achieve.
Take a recent case we had with an agricultural equipment client. They sent us forged gear blanks, and initially, our team focused only on getting the tooth profile within 0.001 inches of tolerance. But when they tested the first batch, three gear teeth cracked after just 100 hours of use. We went back to check our process and realized we’d been using a dull end mill to finish the tooth roots. The dull tool wasn’t cutting the metal cleanly—it was actually smearing it, creating a rough surface with high residual tensile stresses right at the tooth’s root, which is the highest-stress point on a gear. Once we switched to a sharp, coated carbide tool and adjusted our feed rate, the next batch of gears ran for over 1,500 hours without a single crack. That’s when I really realized: surface integrity isn’t a “nice to have” for machined forging parts—it’s the make-or-break requirement.
First and foremost, there’s the surface roughness requirement, and it’s not one-size-fits-all. Let’s be clear: a rough surface is never bad, but a rough surface in the wrong place is a disaster. For machined forging parts, the roughness (measured as Ra, or average roughness, and Rz, or maximum peak-to-valley height) is tailored to the part’s application. For critical aerospace turbine blades, for example, we need an Ra value of less than 0.8 micrometers because even a tiny peak can act as a stress raiser that leads to fatigue failure at high temperatures. For construction equipment hydraulic fittings, we might allow a higher Ra—around 1.6 micrometers—because the parts are under less cyclic stress, and a slightly rougher surface is fine for sealing. The key here is that we never use a generic roughness spec; we work with each client to map the part’s load zones and set roughness targets only for those areas that will see high stress or friction.
But roughness alone doesn’t tell the whole story. The second big requirement is residual stress state. When you machine a forging, the cutting tool generates heat and force that deforms the top layers of the part. If that deformation leaves tensile residual stresses, that’s bad—tensile stresses add to the working stresses the part will see in use, making it much more likely to crack or fail under cyclic loading. What we want is compressive residual stresses in the surface layers, because those actually counteract the working tensile stresses the part will face. How do we get that? It’s all in our machining parameters. We learned early on that using too high a cutting speed or too low a feed rate can create excess heat that softens the surface and leaves tensile stresses. Now, for most carbon steel forgings, we stick to a cutting speed of around 150-200 surface feet per minute (SFM) and a feed rate of 0.003-0.005 inches per tooth for finishing passes. For harder alloy forgings, we adjust to slower speeds and heavier feeds to keep heat generation low. We also use cryogenic machining for some high-stress parts—blasting the cutting zone with liquid nitrogen to keep the surface cool, which actually introduces mild compressive stresses as the part cools evenly. That’s a game-changer for parts that will be exposed to thousands of load cycles, like automotive crankshafts.
Next up: microstructure preservation. Forgings have a fine, uniform grain structure (if done right) that gives them their strength and toughness. But machining can alter that top 0.001 to 0.010 inches of the surface. If the cutting tool is too sharp or the heat is too high, it can cause grain refinement (making grains smaller than they should be) or grain growth (making them larger), or even create a deformed layer called a “white layer” because it’s invisible under normal microscope lighting. That white layer is brittle, and it’s a common cause of early fatigue failure. A few months ago, we got a rush order for forged connecting rods for a performance racing engine. The client’s original machinist had created a white layer on the rod’s bolt holes during finishing, and after dyno testing, three rods broke at the bolts. We re-machined the holes using a low-heat process that left no white layer, and those rods went on to win races. That experience taught us we have to test for microstructure changes on every critical part, not just assume our machining process isn’t damaging the forging’s grain structure. We now use optical microscopy and microhardness testing on sample parts from every production run to ensure the surface microstructure matches the original forging’s specification.
Then there’s the often-overlooked requirement of surface anomaly control: microcracks, smearing, burrs, and leftover forging scale that wasn’t removed during machining. Microcracks are especially dangerous because they’re tiny—sometimes just a few micrometers long—but they act as stress raisers that propagate quickly. We once had a client in the wind energy sector who complained about forging gear hubs cracking on the flange. When we inspected the parts, we found microcracks along the flange’s machined edge, caused by using a too-aggressive chamfering tool that dragged the metal instead of cutting it. We switched to a smaller, sharper chamfer tool and adjusted the tool path to cut in both directions, eliminating those microcracks. For burrs, even tiny ones on threaded holes can cause assembly issues or create stress concentrations when the part is tightened, so we use a combination of deburring brushes, ultrasonic cleaning, and hand deburring for critical threaded and mating surfaces.
Wait, let’s also talk about how material type affects all these requirements. Not all forgings are the same, right? We machine everything from low-carbon steel for agricultural parts to titanium alloys for aerospace and high-nickel alloys for power generation parts. For titanium forgings, for example, surface integrity is extra tricky because titanium has a low thermal conductivity—so all the heat from machining stays right at the surface, leading to higher residual stresses and a higher risk of microcracks. For titanium parts, we use tools coated with diamond-like carbon (DLC) that reduces friction, and we machine at slower speeds with higher air pressure to blow away chips and cool the cutting zone. For high-nickel alloys, which are hard and work-harden quickly, we use constant cutting forces to avoid smearing the surface, which would alter the grain structure.
Now, I know what a lot of clients ask me: “Why can’t we just use a grinding machine to get a perfect surface?” Grinding works for some parts, but for forged parts, especially those with complex shapes, grinding can introduce similar or even worse residual stresses. Our shop uses a mix of turning, milling, and abrasive finishing, depending on the part’s needs. For parts that need extremely smooth surfaces with high compressive stresses, we sometimes use a process called burnishing, where a hard rolling tool is pressed against the freshly machined surface to smooth it and compress the surface layers, adding that extra compressive stress that’s so good for fatigue life. Burnishing is perfect for parts like bearing races, where a smooth, stress-free surface is critical for long life.
Another key requirement is consistency across production runs. It’s not enough for one batch of parts to have good surface integrity—every single part has to meet the same specs. That’s why we have a strict quality control process that checks surface roughness on 100% of critical parts, tests residual stresses on 5% of each batch, and does microstructure checks on 1% of parts. We also use in-process monitoring tools—like tool wear sensors that track how dull our cutting tools get, so we replace them before they start damaging the surface. A few years ago, we had a batch of forged hydraulic cylinders where a set of tools wore out faster than expected, and our tool wear sensor caught it before we produced a whole bad batch. That saved our client from costly downtime and kept our reputation intact.
Let’s circle back to that agricultural gear case I mentioned earlier. The client told us that before they started working with our shop, they were having a 12% failure rate on their gears due to surface-related issues. After we adjusted our machining process to focus on surface integrity, that failure rate dropped to less than 1%. That’s the difference we’re talking about here. Machining a forging isn’t just about cutting it to the right size—it’s about preserving all the strength and durability that the forging process created, and that starts and ends with the surface.
Now, if you’re in the market for machined forging parts, or if you’re dealing with parts that are failing prematurely, it’s worth asking your supplier about their surface integrity requirements. Don’t just ask for a tolerance on dimension or a surface roughness number—ask about their process for controlling residual stresses, testing for microstructure changes, and preventing microcracks. That’s where the good suppliers separate themselves from the ones who just push parts through a machine and call it done.
At our shop, we don’t just see ourselves as a forging part machining supplier—we see ourselves as partners in making parts that last. We’ve spent years refining our processes, learning from every problem and every success, because we know that a part that works as intended is the best advertisement we can have.
If you’re working on a project that needs machined forging parts, whether it’s for automotive, aerospace, agriculture, construction, or any other industry, and you want to make sure surface integrity is on point, we’d love to talk through your requirements. We can take your forged blanks, machine them to your exact specs, and ensure that every surface meets the strict standards that our clients have come to rely on. No generic processes, no cutting corners—just high-quality machined forging parts that perform when you need them to.
CNC Milling Service References
- Davim, J. P. (2010). Surface Integrity in Machining. Springer.
- Field, M., & Kahles, J. F. (1971). The Surface Integrity of Machined Components. Annals of the CIRP, 20(2), 227-246.
- Trent, E. M., & Wright, P. K. (2000). Metal Cutting (4th ed.). Butterworth-Heinemann.
- Astakhov, V. P., & Xiao, X. (2011). Surface Integrity in Machining: Theory and Applications. CRC Press.
Ningbo Yirui Machinery Manufacturing Co., Ltd.
As one of the most professional forging part machining manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to wholesale durable forging part machining made in China here from our factory. Customized orders are welcome.
Address: No.107, Wanzhong Village, Jishigang Town, Haishu District, Ningbo City
E-mail: James.he@yiruitek.com
WebSite: https://www.yiruime.com/
